High Molecular Weight PAM Flocculant | Superior Water Treatment

showlist/high-molecular-weight-pam-flocculant, showlist/high-molecular-weight-pam-flocculant, 
Inquiry
showlist/high-molecular-weight-pam-flocculant, showlist/high-molecular-weight-pam-flocculant, 
Inquiry
High Molecular Weight PAM Flocculant for Superior Water Treatment

High Molecular Weight PAM Flocculant for Superior Water Treatment

High molecular weight PAM flocculant, or polyacrylamide, is a cornerstone in modern water treatment and solid-liquid separation processes. At Jiangsu Feymer Technology Co., Ltd., we engineer high molecular weight PAM flocculant with exceptional chain length and anionic, cationic, or nonionic characteristics to meet the diverse demands of industries such as pulp and paper manufacturing, oil and gas recovery, fine chemical production, textile dyeing, and both industrial and municipal wastewater treatment. Our high molecular weight PAM flocculant solutions are designed to accelerate particle aggregation, enhance settling rates, and improve sludge dewatering efficiency, resulting in clearer effluents and reduced operational costs. Leveraging our facilities and our listing on China’s STAR Market, we provide a consistent, high-quality supply of high molecular weight PAM flocculant backed by rigorous quality control and a dedicated technical support team.
Get A Quote

Advantages of the product

Enhanced Flocculation Efficiency

Our high molecular weight PAM flocculant is specially synthesized to offer superior bridging and charge neutralization capabilities. This results in rapid micro-floc formation and macro-floc aggregation, dramatically improving settling and filtration rates. Industries benefit from reduced retention times and smaller footprint treatment systems, leading to significant energy and space savings. The high molecular weight ensures that even low dosages are effective, reducing chemical consumption and cost. Whether you’re clarifying raw water, thickening sludge, or dewatering industrial slurries, this flocculant delivers consistency and high performance that surpasses conventional alternatives.

Versatile Ionic Variants for Tailored Applications

We offer our high molecular weight PAM flocculant in anionic, cationic, and nonionic forms, each engineered to address specific water chemistry and particulate characteristics. Anionic PAM excels in treating inorganic suspensions and is widely used in mining and mineral processing. Cationic PAM is ideal for organic-rich sludge generated by municipal and food processing industries, improving dewatering to reduce disposal costs. Nonionic PAM bridges a broad spectrum of applications, offering optimal performance where charge density is low or variable.

Superior Dissolution and Economic Dosage

Our high molecular weight PAM flocculant is produced using advanced manufacturing techniques that yield a product with excellent water solubility, reducing make-down time and eliminating fish-eye formations. The ultra-high molecular weight facilitates strong floc structures that are shear-resistant, helping to maintain performance even in turbulent environments. Because of its high efficiency, less polymer is needed to achieve target clarity and dewatering results, directly lowering your chemical costs. Additionally, the polymer’s stability across a wide pH range and temperature conditions ensures consistent performance year-round, minimizing process interruptions.

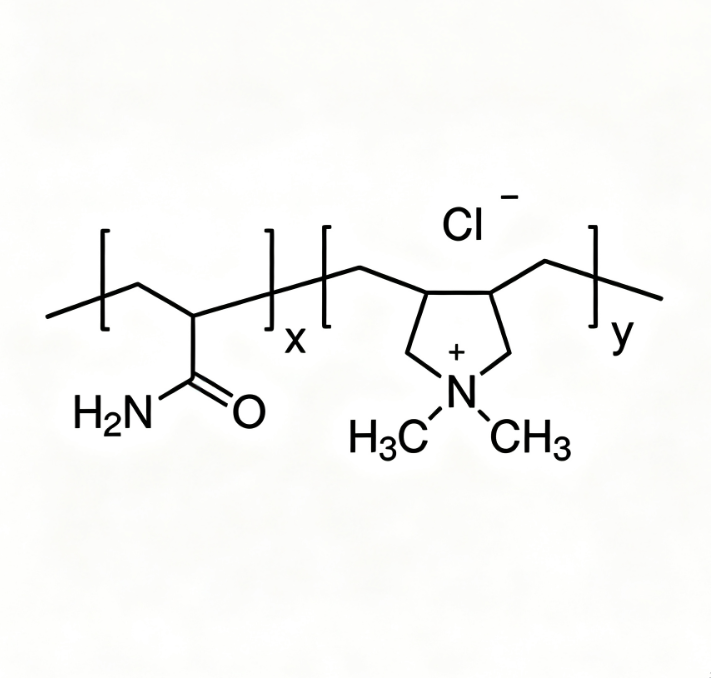
High molecular weight PAM flocculant is a powerful tool for modern water treatment challenges. Water scarcity and tightening discharge regulations necessitate efficient and cost-effective solutions. PAM, an abbreviation for polyacrylamide, is a versatile polymer used extensively in flocculation, sedimentation, and sludge processing. Its name “high molecular weight” refers to polymer chain lengths that often exceed 10 million Daltons, giving it exceptional bridging capabilities. When added to wastewater, the polymer molecules attach to multiple particles, forming larger aggregates that settle faster and filter more easily. This mechanism not only improves clarity but also enhances the efficiency of clarifiers and belt presses. In industrial applications, high molecular weight PAM aids in recovering valuable resources from process streams, conserving water, and minimizing waste volumes. Our factory employs state-of-the-art polymerization methods to produce consistently superior PAM, with controlled viscosity and dissolution rates. We understand that each industry presents distinct water matrices. 

Frequently Questions

What is the difference between high molecular weight PAM flocculant and standard polyacrylamide?

High molecular weight PAM flocculant refers to polyacrylamide with an average molecular weight typically exceeding 10 million Daltons, while standard grades may have lower molecular weights (e.g., 2-5 million). The higher molecular weight results in longer polymer chains that provide more effective bridging between particles. This leads to the formation of larger and stronger flocs, which settle or dewater more rapidly. Consequently, high molecular weight PAM can achieve the same clarity with lower dosages, reducing chemical costs and sludge volume for disposal. Additionally, high molecular weight polymers often exhibit superior resistance to shear forces, maintaining their performance in high-flow systems. The choice between high and standard molecular weight depends on your specific process conditions, such as suspended solids concentration and mixing energy.
While high molecular weight PAM flocculant is widely used in industrial and municipal wastewater treatment, its application in potable water production is subject to local regulations. Many water treatment facilities use food-grade polyacrylamide, which is approved for drinking water with strict purity criteria, including low residual acrylamide monomer content. Our high molecular weight PAM flocculant can be supplied in grades meeting these standards, including NSF/ANSI 60 certification if required. When used correctly and at regulated dosages, it effectively removes turbidity and microorganisms, enhancing the safety of drinking water. However, dosing and flocculation must be carefully controlled to avoid excessive polymer carryover.

Related Articles

Why Use Anionic Polyacrylamide in Mining?

14

Aug

Why Use Anionic Polyacrylamide in Mining?

Discover how anionic polyacrylamide enhances mineral processing efficiency, improves water recovery, and optimizes solid-liquid separation in mining operations.
View More
How Anionic Polymer Improves Solid-Liquid Separation

19

Aug

How Anionic Polymer Improves Solid-Liquid Separation

Discover how anionic polymer improves solid-liquid separation, accelerates settling, and reduces operational costs. Expert manufacturing and supply by Feymer.
View More
Anionic Polyacrylamide for Mineral Tailings

19

Aug

Anionic Polyacrylamide for Mineral Tailings

Discover how high-performance anionic polyacrylamide optimizes tailings dewatering for mines. Improve efficiency and sustainability with Feymer solutions.
View More

Customer Testimonials

Sarah Chen
Revolutionized Our Sludge Dewatering Process

Using Feymer’s high molecular weight PAM flocculant at our municipal plant reduced our sludge drying time by 30% and cut polymer costs by 20%. The product dissolves easily, and our operators appreciate the consistent quality. Even during peak load conditions, the floc formation is excellent, and our effluent meets stringent discharge limits.

Michael Nguyen
Outstanding Performance in Oil-Water Separation

As a senior water specialist in the oil sands industry, I have tested numerous PAM products. Feymer’s high molecular weight PAM flocculant outperforms others in terms of floc strength and settling rate. We now treat higher volumes with lower dosages, translating to significant cost savings. The technical support team was responsive and provided excellent guidance during our trials.

Get a Free Quote

Our representative will contact you soon.
0/1000
Proven Track Record and Market Leadership

Proven Track Record and Market Leadership

Jiangsu Feymer Technology Co., Ltd. has cultivated a reputation as a leading supplier of water treatment chemicals since its inception in 2010, culminating in our public listing on China’s STAR Market in 2021. Our high molecular weight PAM flocculant is the result of years of research and process optimization, embodying our commitment to quality and innovation. We operate three production bases and five factories across Jiangsu and Anhui, ensuring robust supply chains that can scale to meet client demands. Our technical team’s expertise allows us to provide tailor-made solutions, whether for large-scale utilities or specialized industrial processes. By choosing us, you partner with a company that understands the importance of reliability and performance. Our high molecular weight PAM flocculant has successfully been deployed in various sectors, from pulp and paper to oil and gas, resulting in improved efficiencies and reduced environmental footprints.
Cutting-Edge Manufacturing and Quality Assurance

Cutting-Edge Manufacturing and Quality Assurance

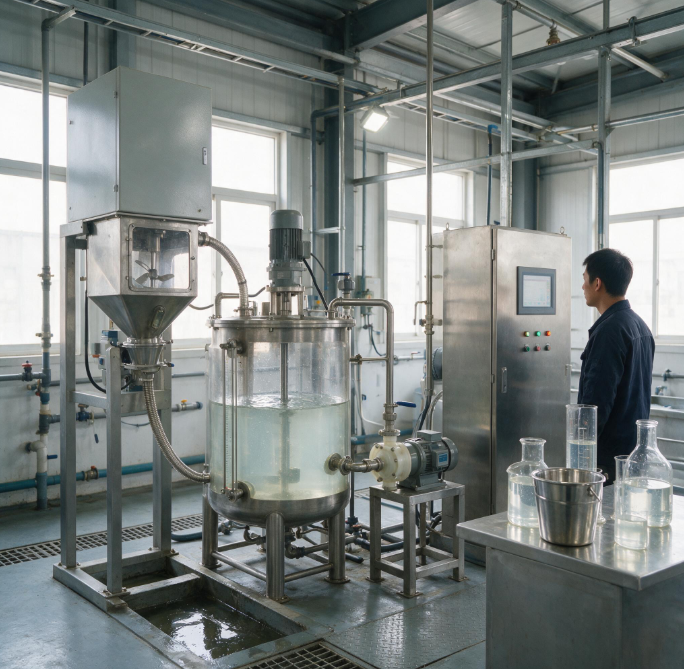
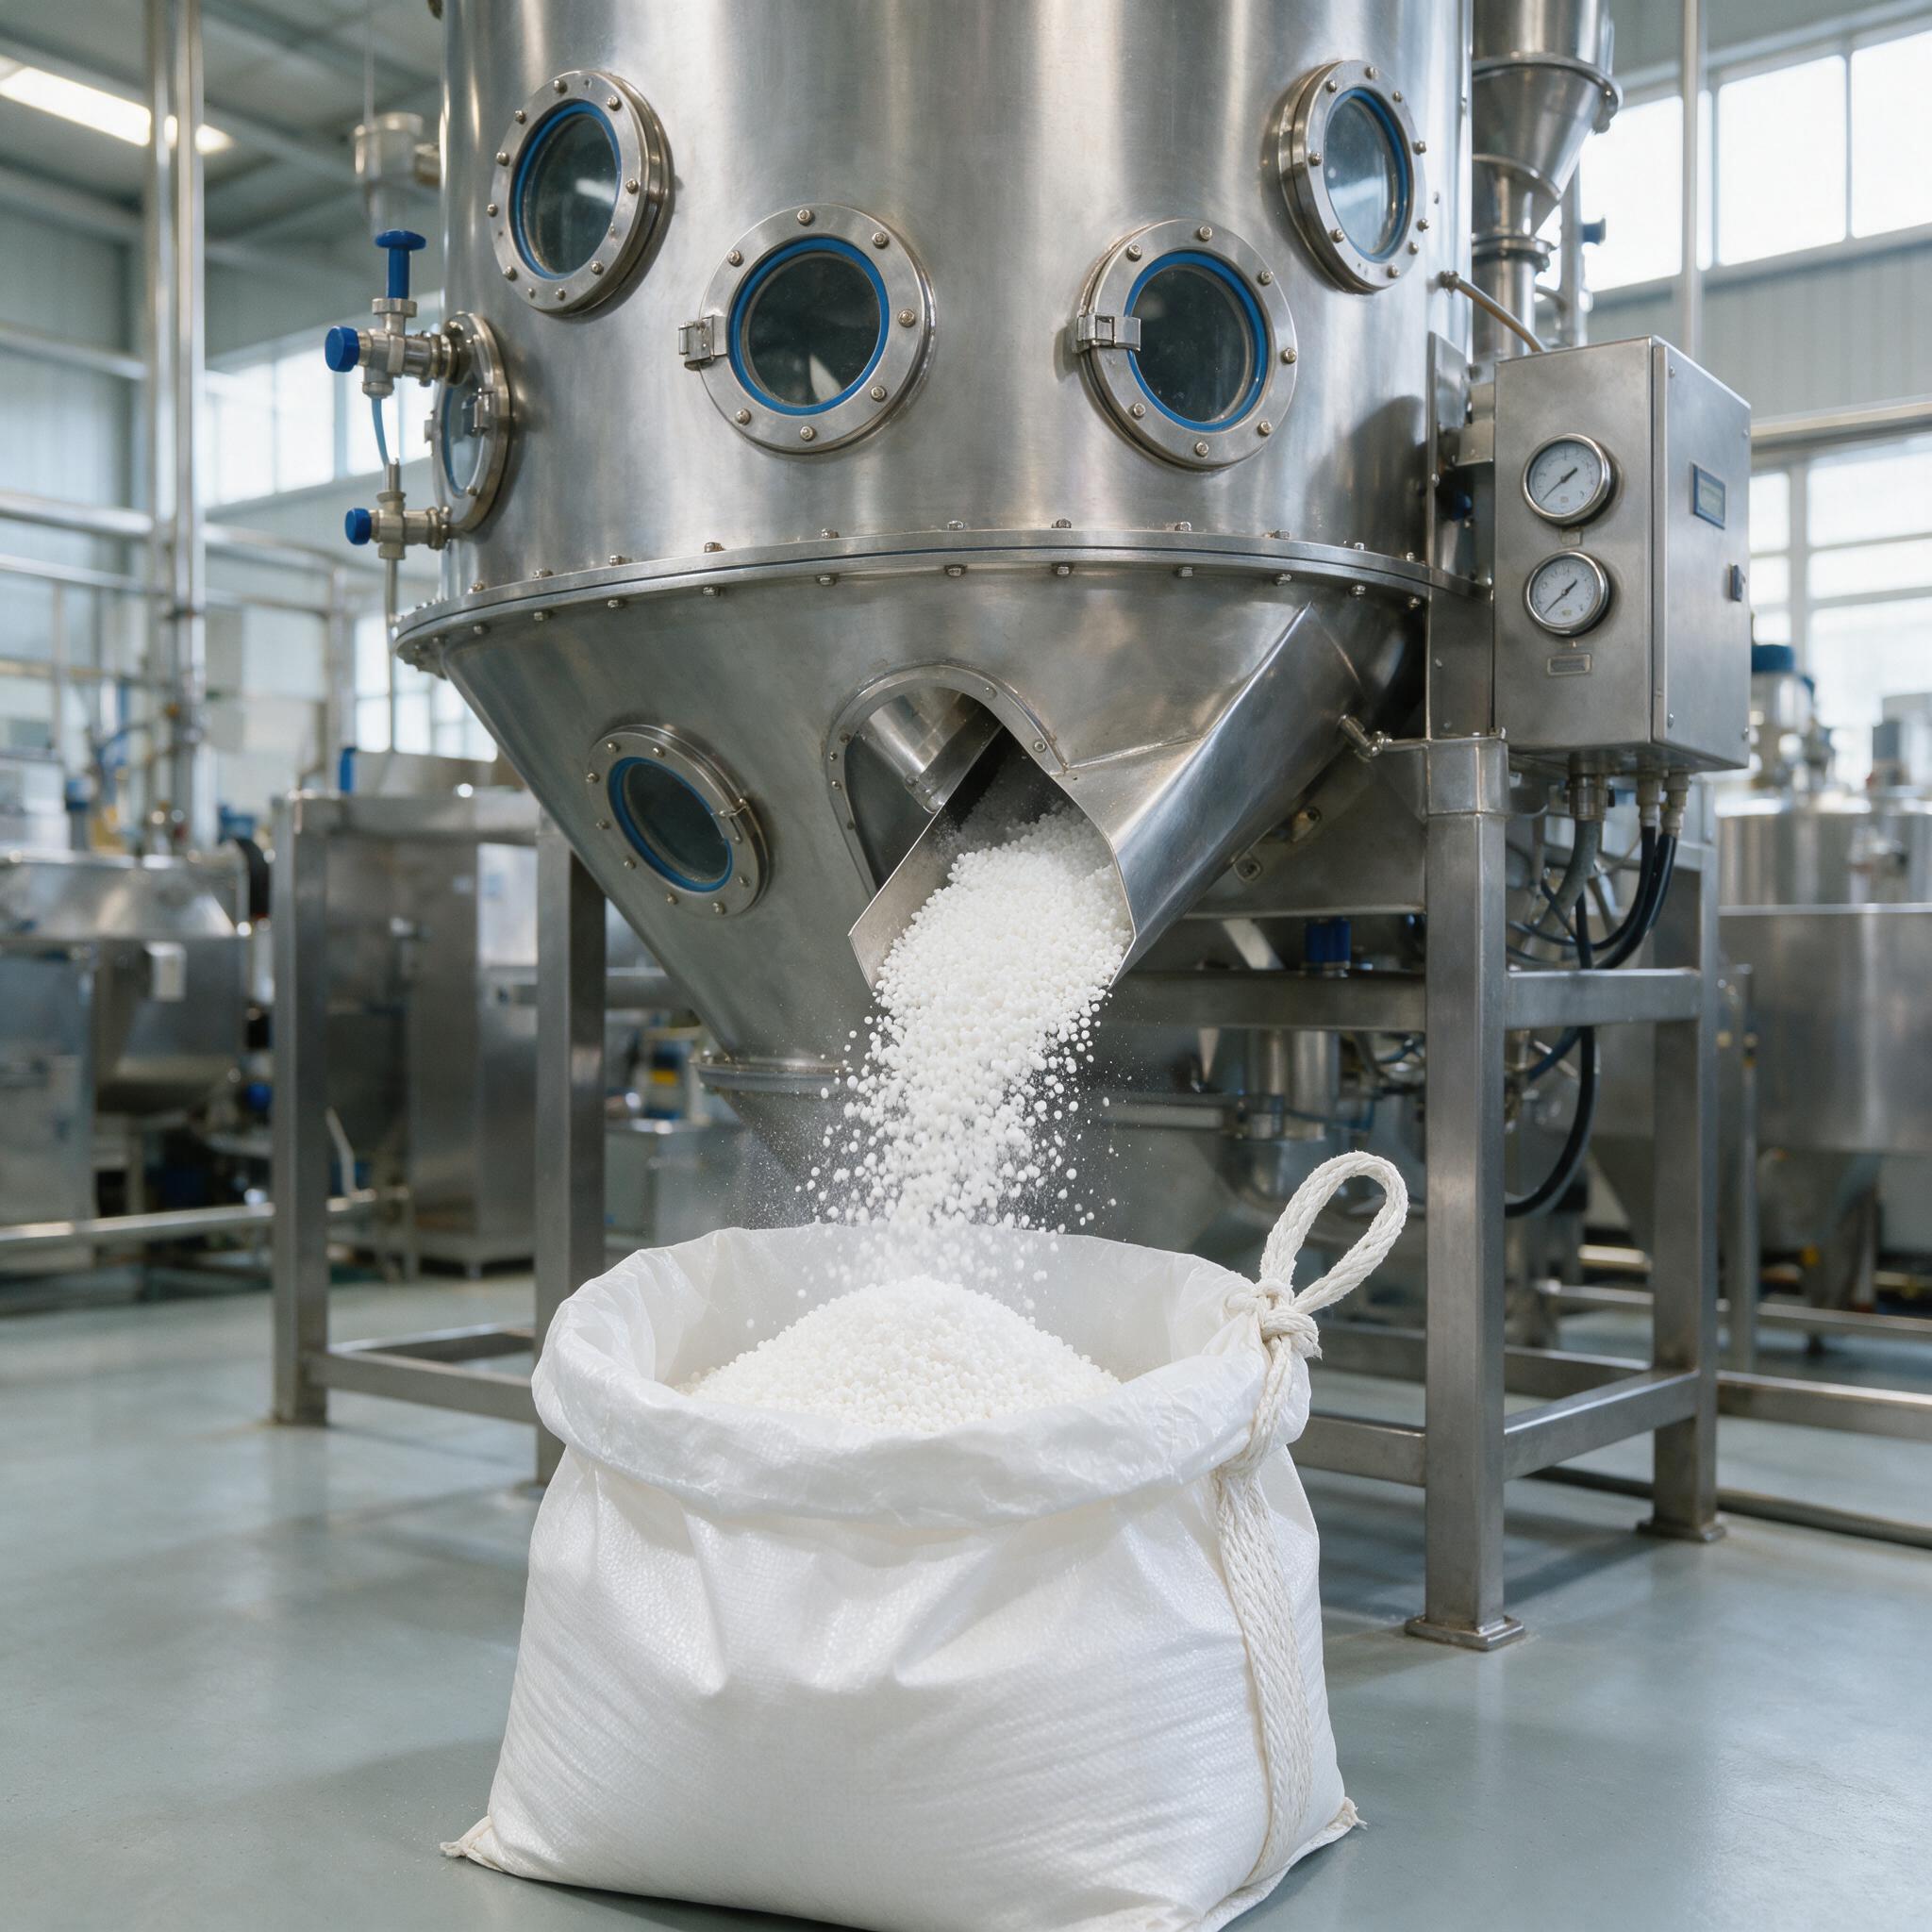
Our high molecular weight PAM flocculant is produced using the latest polymerization technologies in fully automated facilities, ensuring batch-to-batch consistency and high dissolution rates. We adopt rigorous quality control measures at every stage of production, from raw material selection to final packaging. Each batch undergoes comprehensive testing for molecular weight, charge density, and residual monomer content, guaranteeing that our flocculant meets or exceeds industry specifications. We also provide a certificate of analysis with every shipment. This quality assurance minimizes risks for your operations and gives you predictable performance. Additionally, our R&D team continuously explores ways to improve polymer efficiencies, ensuring that we stay ahead of environmental regulations while delivering a product that enhances your productivity.