PAM Chemical Factory & Polyacrylamide Manufacturer

showlist/pam-chemical-factory, showlist/pam-chemical-factory, 
Inquiry
Inquiry
Leading PAM Chemical Factory | Sustainable Water Treatment Solutions

Leading PAM Chemical Factory | Sustainable Water Treatment Solutions

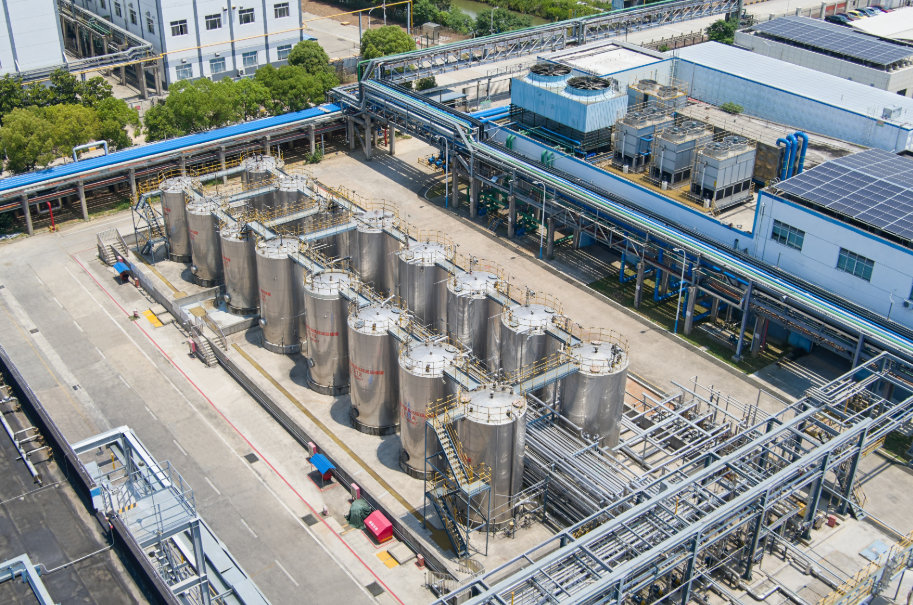
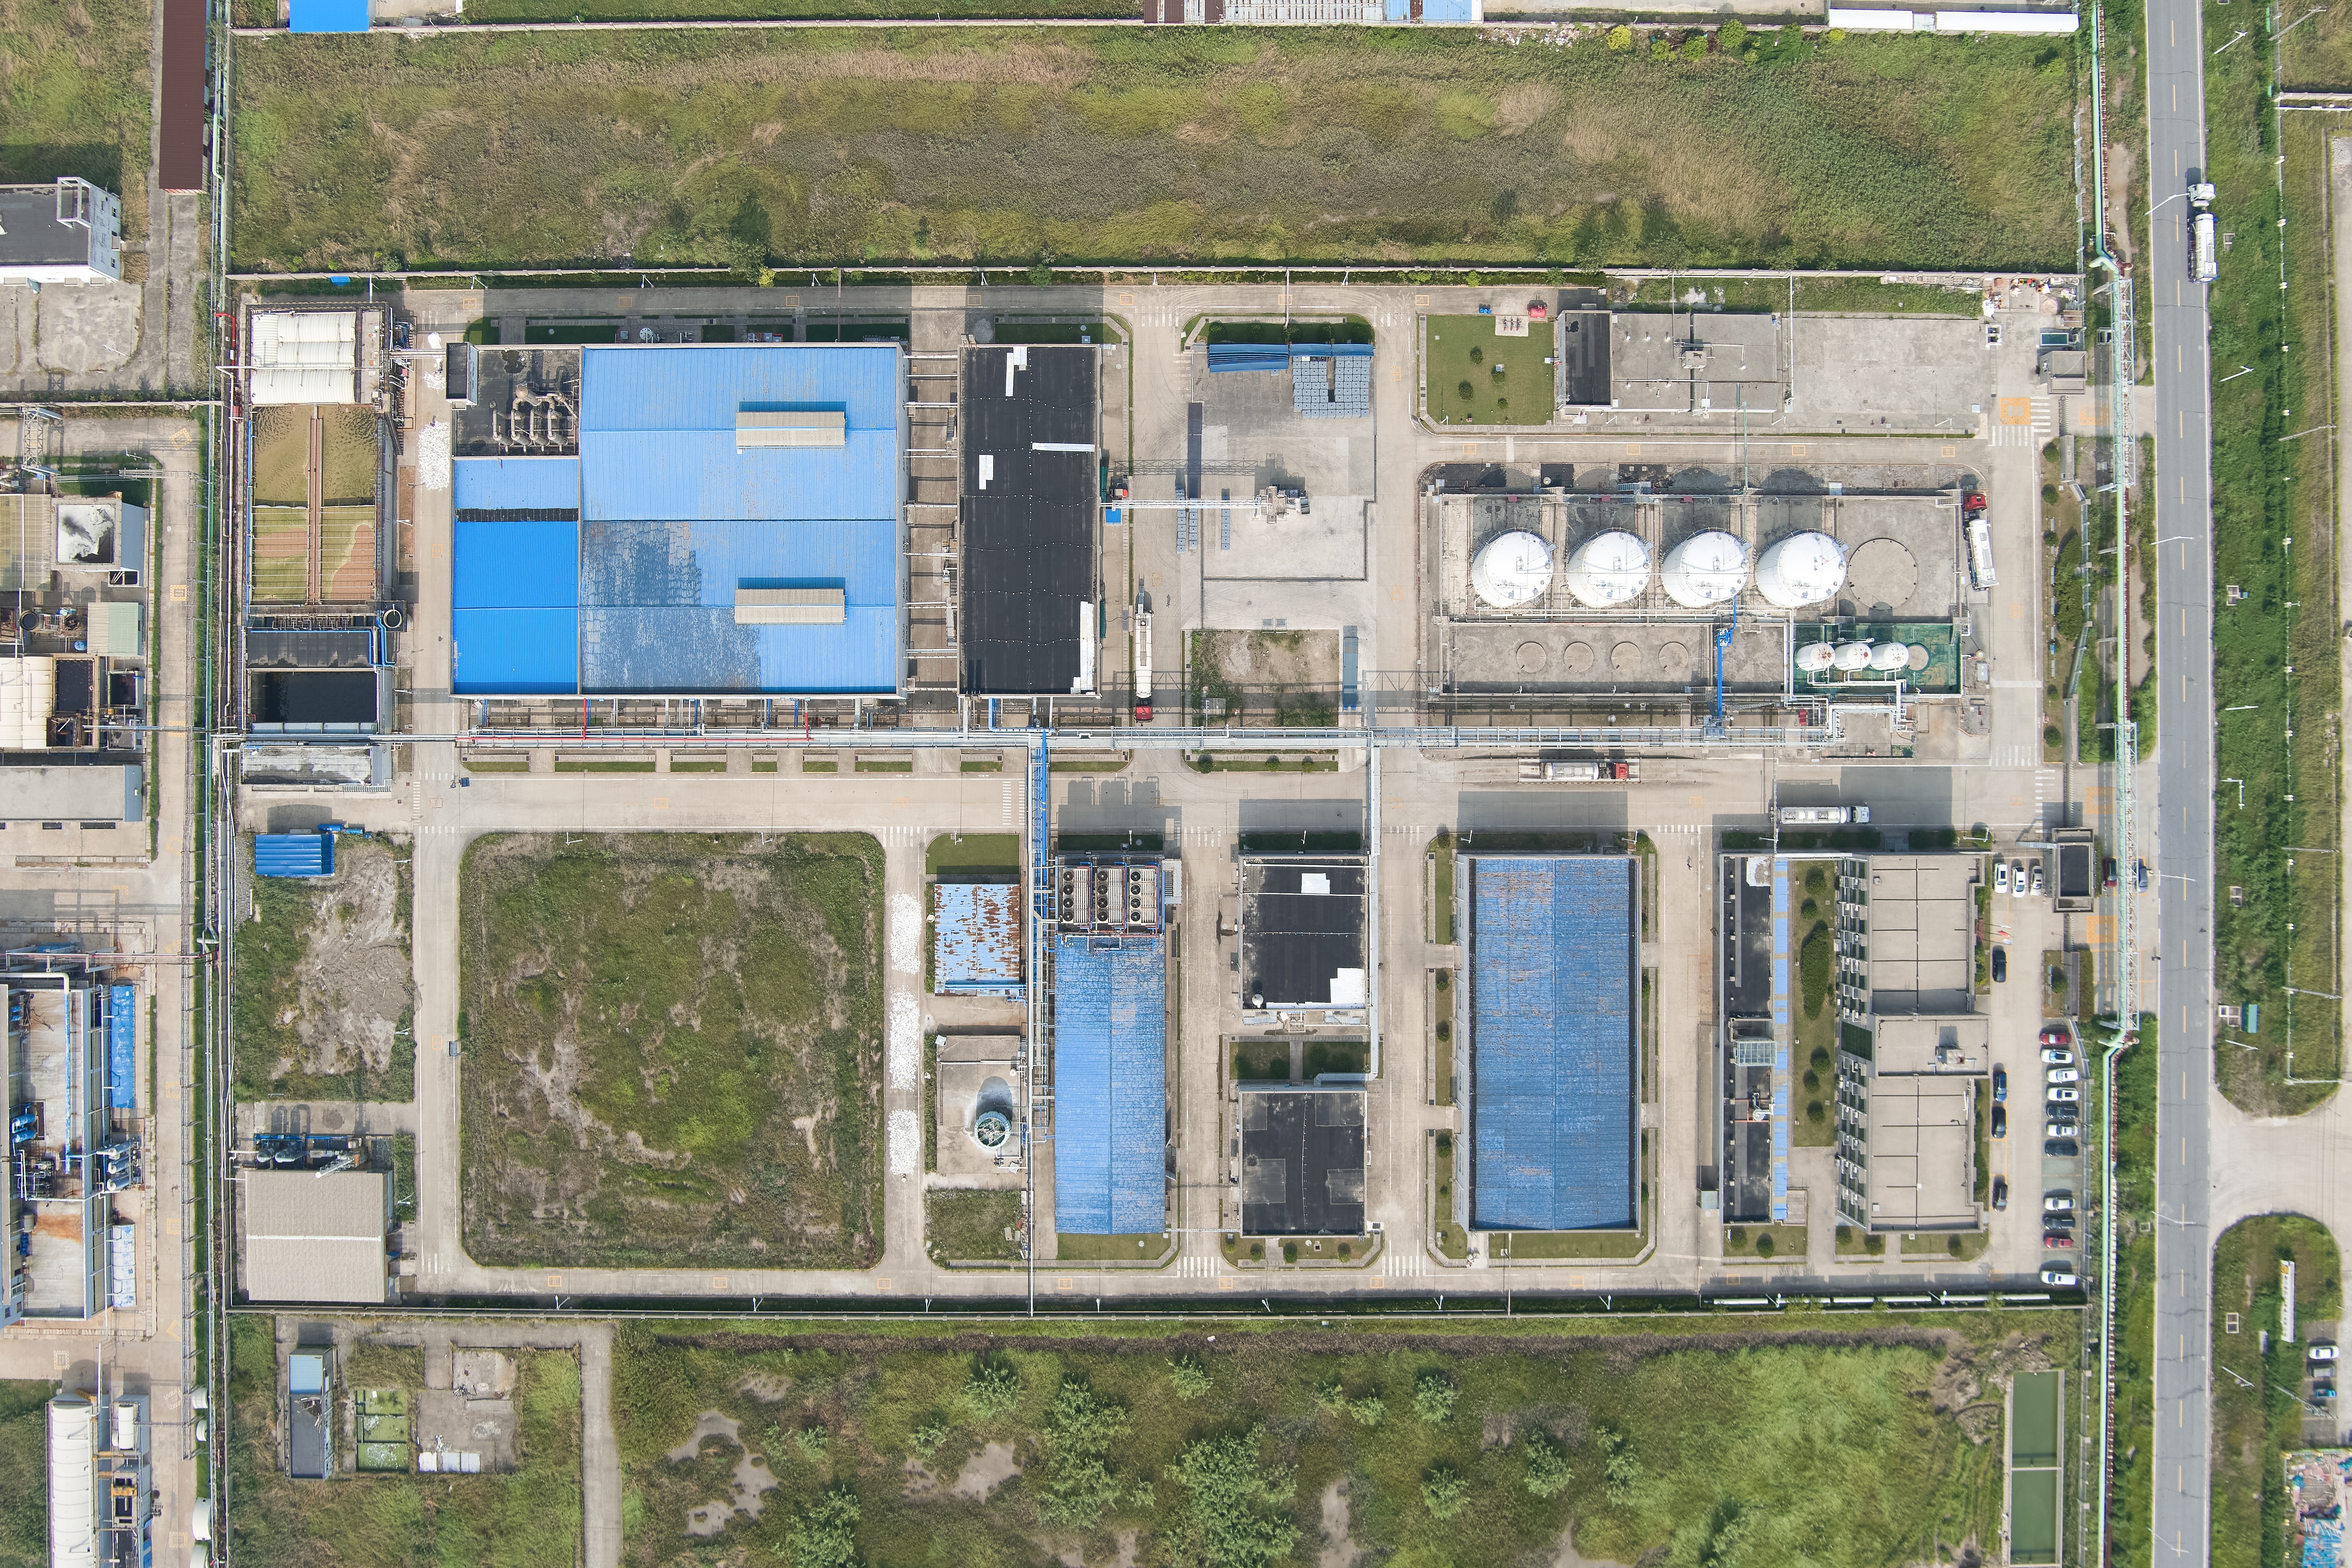
Welcome to Jiangsu Feymer Technology Co., Ltd., a premier PAM chemical factory dedicated to advancing water treatment technologies. As a high-tech enterprise listed on China’s STAR Market, we specialize in the production of polyacrylamide (PAM) and other water-soluble polymers that cater to diverse industries including pulp and paper, oil & gas, textile dyeing, and municipal water treatment. Our commitment to sustainability is embodied in our mission, ‘Making Every Waterprint Count,’ which drives our innovation in functional monomers and membrane technologies. With three production bases and five factories across Jiangsu and Anhui, we ensure reliable supply and consistent quality. Our advanced R&D capabilities enable us to offer customized solutions that meet the most demanding specifications.
Get A Quote

Advantages of the product

Advanced Manufacturing and Quality Control

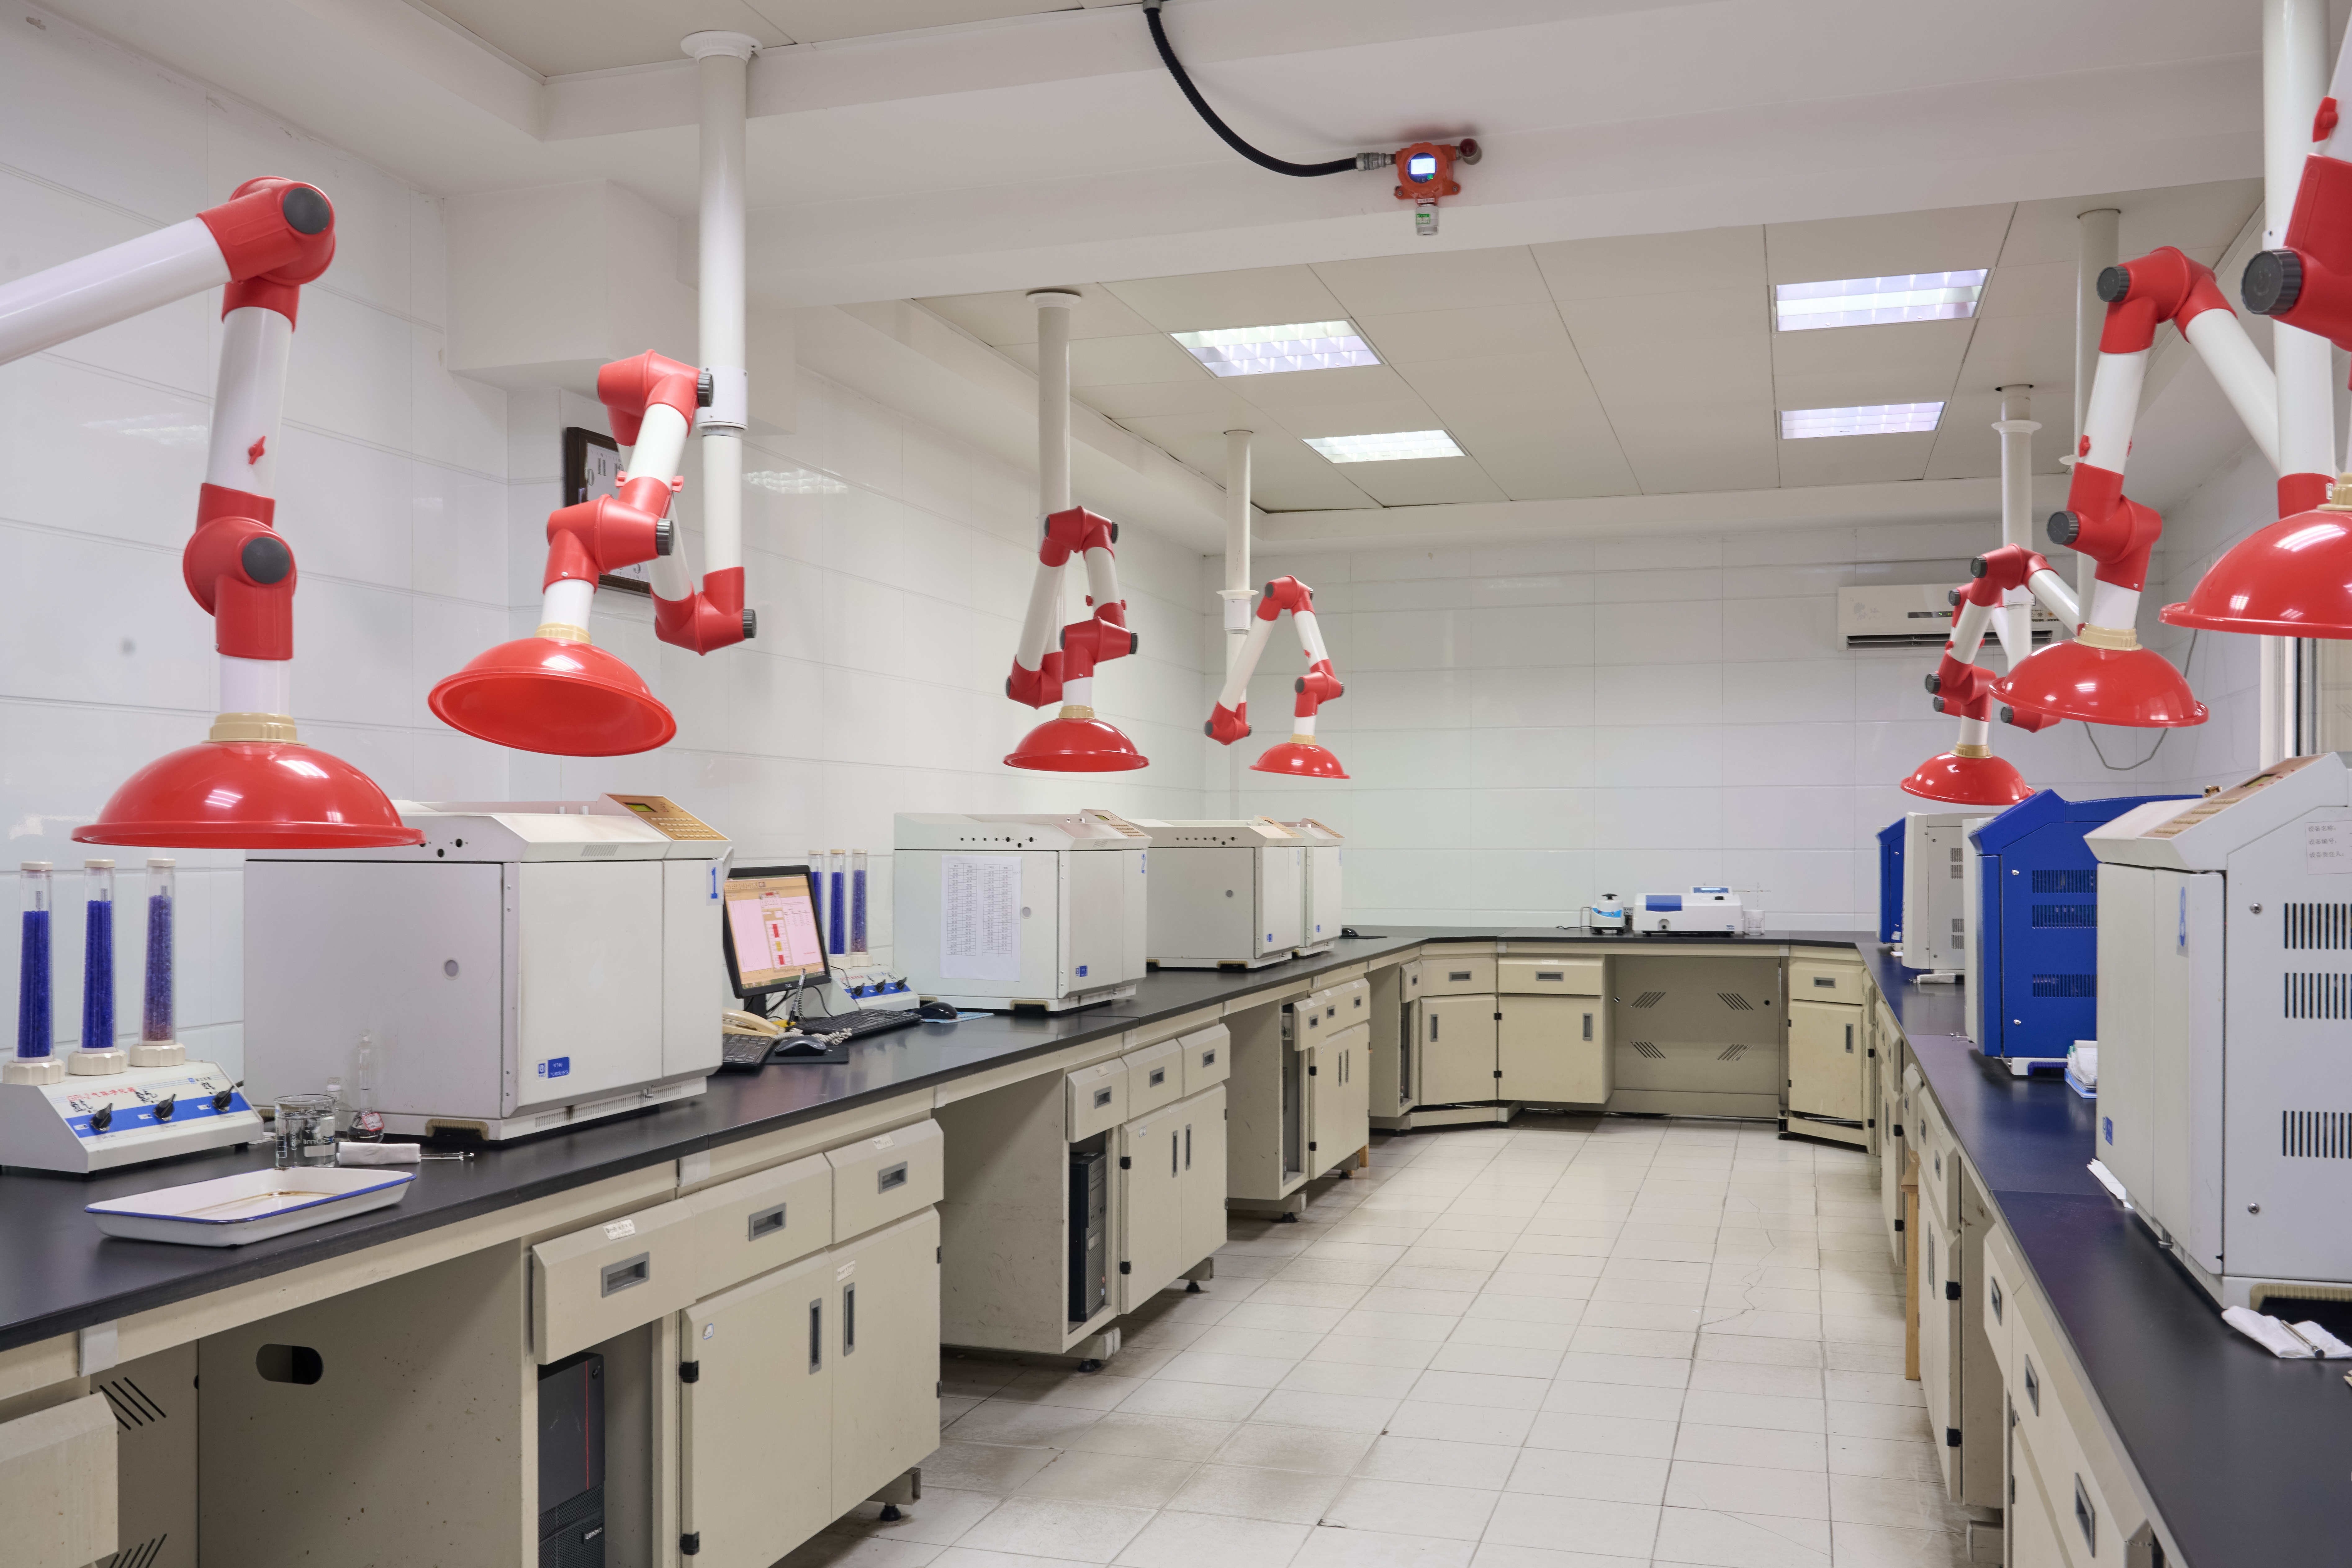
Our PAM chemical factory is equipped with cutting-edge production lines that utilize automated control systems and advanced polymerization technologies. We maintain rigorous quality management systems that span from raw material sourcing to final product delivery. Each batch undergoes comprehensive testing in our accredited laboratories, ensuring that our PAM products meet international standards such as ISO 9001 and ISO 14001.

Customization and Technical Support

We understand that every water treatment challenge is unique. Our team of experienced engineers and scientists works closely with clients to develop customized PAM formulations tailored to their specific water chemistry, process conditions, and performance requirements. Whether you need a high molecular weight polymer for enhanced flocculation or a low charge density product for specialized filtration, we can modify molecular weight, ionic charge, and degree of hydrolysis to achieve the desired outcomes.

Commitment to Sustainability and Innovation

As an industry leader, our PAM chemical factory integrates sustainability into every aspect of our operations. We utilize environmentally friendly production processes that minimize energy consumption and waste generation. Our products are designed to facilitate water recycling and reduce sludge volumes, contributing to circular economy principles. Additionally, we invest heavily in research and development to innovate next-generation PAM derivatives that are biodegradable and have lower environmental footprints.

Polyacrylamide (PAM) is a synthetic polymer that has become indispensable in modern water treatment processes. As a leading PAM chemical factory, we produce a comprehensive range of PAM products that address various challenges in liquid-solid separation. PAM functions by neutralizing the charge of suspended particles and bridging them into larger flocs, which can then be easily removed by sedimentation or filtration. This mechanism is crucial in reducing chemical oxygen demand (COD), biochemical oxygen demand (BOD), and total suspended solids (TSS) in industrial and municipal wastewater. In sludge dewatering applications, cationic PAM is particularly effective. It conditions sludge by destabilizing the colloidal system, allowing for mechanical dewatering through belt presses or centrifuges. The result is a drier sludge cake with lower volume, which significantly reduces disposal costs.

Frequently Questions

What factors should I consider when selecting a PAM product for my wastewater treatment?

Selecting the appropriate polyacrylamide (PAM) for your wastewater treatment system is crucial to achieving efficient and cost-effective results. Key factors include the type of contaminants in your water, the pH level, the charge of the suspended particles, and the equipment you use for mixing and dewatering. First, identify whether your wastewater contains inorganic particles, organic matter, or both. Inorganic particles often require anionic PAM, while organic suspensions typically respond better to cationic PAM. Nonionic PAM can be used in neutral pH environments where both types may be present. The charge density and molecular weight also influence flocculation performance; higher molecular weight increases bridging capability but may lead to slower dissolution.
PAM offers several advantages over traditional inorganic flocculants such as alum and ferric chloride. Organic polymers like PAM are effective at much lower doses, typically requiring only a few parts per million, whereas inorganic coagulants need hundreds of parts per million to achieve similar results. This efficiency translates to reduced chemical costs and lower sludge generation, decreasing downstream disposal expenses. PAM is particularly suited for treating high-strength industrial wastewaters where inorganic coagulants may be ineffective due to high alkalinity. Additionally, PAM can be manufactured with specific charge and molecular weight to address unique water chemistry, offering greater versatility.

Related Articles

Common Industrial Applications of Water Soluble Polymer

21

Jul

Common Industrial Applications of Water Soluble Polymer

Explore industrial applications of water soluble polymer technology. Feymer provides high-purity polymer solutions for water treatment, papermaking, and extraction.
View More
How to Use Anionic Polyacrylamide Correctly?

30

Jul

How to Use Anionic Polyacrylamide Correctly?

Learn how to use anionic polyacrylamide correctly for water treatment. Feymer provides expert guidance and high-performance polymer solutions.
View More
What Are DADMAC Applications in Industry?

04

Sep

What Are DADMAC Applications in Industry?

DADMAC applications span water treatment, paper manufacturing, textiles, and oilfield chemistry. Explore how this cationic monomer serves industry.
View More

Customer Testimonials

Nguyen Tran
”Exceptional Quality and Outstanding Support

Our engineering team at the municipal water treatment plant in Vietnam has been using Feymer’s PAM for over two years. The product quality has been consistently high, with excellent dissolution and effective flocculation, which significantly improved our settling tank performance. The sludge volume has decreased by 30% compared to the previous chemical we used, and we’ve achieved lower turbidity levels in the final effluent. What sets them apart is their excellent technical support.

Md. Rahim
”Reliable Partner for Industrial Effluent Treatment

As a mid-sized textile dyeing and finishing unit in Bangladesh, we struggled with meeting environmental discharge standards due to high color and organic load in our effluent. After consulting various suppliers, we switched to Feymer’s PAM chemicals. The products were customized to suit our specific dye and surfactant composition, and the flocculation efficiency was remarkable. The treatment time in our clarifier reduced by half, and we now achieve over 90% color removal, comfortably passing local compliance.

Get a Free Quote

Our representative will contact you soon.
0/1000
Proven Expertise and Market Leadership

Proven Expertise and Market Leadership

As a PAM chemical factory with over a decade of experience, Feymer Technology has established itself as a leading player in the water treatment chemical industry. Our company is listed on China’s STAR Market, a testament to our financial stability and technological innovation. We boast a production capacity of over 100,000 tons per year across our sites, enabling us to meet both small-scale and large-scale orders with agility and consistency. Our R&D center, staffed with over 200 scientists and engineers, holds various patents in polymer synthesis and application technologies. We directly serve more than 1,000 clients across 50 countries, providing tailor-made solutions. This market leadership translates into deep industry insights and a robust supply chain. When you partner with us, you gain access to a wealth of knowledge drawn from thousands of successful projects.
Innovative Production and Sustainable Practices

Innovative Production and Sustainable Practices

Our PAM chemical factory is distinguished by its commitment to environmentally responsible manufacturing. We have implemented closed-loop processes that recycle solvents and reduce waste, achieving a carbon footprint that is 30% lower than conventional factories. Our new production lines feature advanced continuous reactors that increase efficiency and ensure uniform polymer quality. We use bio-based and green crosslinkers, and our PAM grades are available in a ‘Green’ certification line, which uses renewable raw materials and is designed to enhance biodegradability. Innovation is at the core of our operations: we are pioneers in the use of AI-driven process control, which optimizes reaction conditions to maximize yield while minimizing energy consumption. Additionally, we are developing next-generation PAM derivatives with better salt-tolerance and shear resistance, which are crucial for enhanced oil recovery and industrial water treatment under harsh conditions.