PAM Chemical Manufacturer

showlist/pam-chemical-manufacturer, showlist/pam-chemical-manufacturer, 
Inquiry
showlist/pam-chemical-manufacturer, showlist/pam-chemical-manufacturer, 
Inquiry
Leading PAM Chemical Manufacturer | Sustainable Water Treatment Solutions

Leading PAM Chemical Manufacturer | Sustainable Water Treatment Solutions

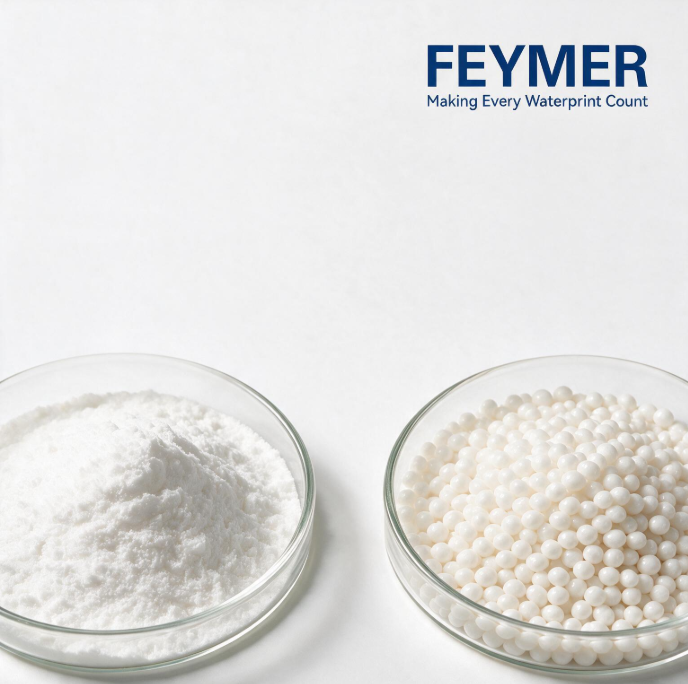
We are a premier PAM chemical manufacturer, specializing in high-performance polyacrylamide (PAM) for water treatment, oil & gas, pulp & paper, and textile industries. As a listed high-tech company on China’s STAR Market (688350), we combine advanced R&D, AI-empowered processes, and eco-friendly production to deliver cost-effective, scalable solutions. Our PAM products—available in anionic, cationic, nonionic, and amphoteric forms—excel in flocculation, dewatering, and sludge conditioning, ensuring compliance with international discharge standards. With three production bases and five factories, we guarantee stable supply and customized formulations to meet client needs. Partner with us for reliable PAM chemicals that enhance efficiency while minimizing environmental impact.
Get A Quote

Advantages of the product

Proven Technological Leadership

Our advantage as a PAM chemical manufacturer lies in our proprietary production technology for functional monomers and water-soluble polymers. With 15+ years of R&D expertise and a strong portfolio of patents, we achieve molecular weights up to 25 million and controlled ionic charges, delivering superior flocculation performance compared to standard products. We employ AI-empowered quality control to monitor every batch, ensuring consistent purity and viscosity. The manufacturing process emphasizes low residual acrylamide, meeting stringent food-safe and environmental standards, such as NSF and REACH.

Reliable Scale and Supply Chain

As a large-scale PAM chemical manufacturer, we operate three state-of-the-art production bases and five factories across Jiangsu and Anhui, with a combined annual production capacity exceeding 200,000 metric tons. This scale ensures uninterrupted supply even during peak demand periods, protecting our customers from market volatility. Our strategic location in the Yangtze River Delta provides access to major logistic hubs, enabling efficient global shipping. We maintain strategic inventory of raw materials to mitigate supply chain risks and ensure fast lead times

Sustainability and Compliance

Sustainability is at the core of our operations, and we are proud to be an eco-friendly PAM chemical manufacturer. Our production processes are designed to minimize energy consumption and waste, utilizing solvent-free and water-based polymerization techniques wherever possible. We actively reduce our carbon footprint and have received certifications such as ISO 14001 and OHSAS 18001, reflecting our commitment to environmental and occupational safety. Our PAM products are designed to be readily biodegradable or have minimal environmental impact in receiving waters, supporting our clients’ sustainability goals.

The role of polyacrylamide (PAM) in modern water treatment cannot be overstated. As a leading PAM chemical manufacturer, we understand that the molecular weight, ionic character, and degree of hydrolysis dictate its efficiency across various applications. Cationic PAM is primarily used for sludge dewatering in municipal and industrial biological treatment plants, where its positive charge neutralizes negatively charged sludge particles, promoting dense floc formation. Anionic PAM excels in mineral processing, coal washing, and drinking water clarification due to its high molecular weight and bridging capabilities. Nonionic PAM is chosen for sensitive environments requiring minimal residual charge, while amphoteric forms offer adaptability to variable influent chemistries.

Frequently Questions

What are the typical applications of PAM from your company?

Our PAM products are extensively used in municipal and industrial wastewater treatment as flocculants, in sludge dewatering, and as process aids in the mining and metallurgy industry (for thickening and filtration). They also serve as retention aids in papermaking, friction reducers in oil and gas well stimulation, and soil conditioners in agriculture (water retention). With our experience as a PAM chemical manufacturer, we can guide you to the optimal grade for your specific application. For instance, anionic PAM is highly effective in treating high-turbidity mineral suspensions, while cationic PAM is preferred for biological sludge. We provide detailed technical datasheets and case studies to help clients from pilot to full scale.
Our PAM products comply with international standards, and we are registered under ISO 9001 for quality management, ISO 14001 for environmental management, and OHSAS 18001 for occupational health and safety. As a reputable PAM chemical manufacturer, we also offer products that meet specific certifications such as NSF/ANSI 60 for drinking water applications and REACH registration for the EU market. We conduct comprehensive quality checks including molecular weight, intrinsic viscosity, residual acrylamide, and dissolution time. We provide certificates of analysis with each shipment and can support you in meeting local regulatory requirements. For special orders, we can arrange third-party inspections (such as SGS or BV) prior to shipping.

Related Articles

Anionic PAM Flocculant for Mineral Tailings Sedimentation

20

Jul

Anionic PAM Flocculant for Mineral Tailings Sedimentation

Improve mineral tailings sedimentation with high-performance anionic PAM. Feymer offers optimized flocculant solutions for efficient mining water recovery.
View More
Why Use Anionic Polyacrylamide in Mining?

14

Aug

Why Use Anionic Polyacrylamide in Mining?

Discover how anionic polyacrylamide enhances mineral processing efficiency, improves water recovery, and optimizes solid-liquid separation in mining operations.
View More
Anionic Polyacrylamide for Mineral Tailings

19

Aug

Anionic Polyacrylamide for Mineral Tailings

Discover how high-performance anionic polyacrylamide optimizes tailings dewatering for mines. Improve efficiency and sustainability with Feymer solutions.
View More

Customer Testimonials

Michael Chen
Exceptional Quality and Cost Savings

We switched to Feymer’s PAM about 18 months ago for our municipal wastewater plant. The anionic grade they recommended has cut our chemical costs by 25% while achieving better effluent clarity. The dissolution time is faster than our previous supplier, which improved operational efficiency. They also provided excellent technical support when we faced seasonal water temperature challenges, offering a custom blend. What’s more, their supply reliability has been fantastic—we never had to worry about stockouts even during peak demand. I highly recommend them as a PAM chemical manufacturer.

Carlos Mendoza
Sustainable Partner for Mining Industry

Our mining operations in South America required a PAM product that could handle high mud content and acidic slurry. Feymer’s technical team analyzed our sample and suggested a high-molecular-weight anionic PAM that outperformed our previous supplier’s product. We observed a 30% reduction in flocculant usage, leading to significant cost savings. They also provided environmental documentation that helped us comply with local regulations. Their logistics team managed the export smoothly, even to remote locations. As a responsible PAM chemical manufacturer, they prioritize sustainability and product safety, which aligns with our corporate values. We appreciate their dedication and long-term commitment to our partnership.

Get a Free Quote

Our representative will contact you soon.
0/1000
Unique Molecular Design

Unique Molecular Design

Our PAM products are synthesized using a proprietary continuous polymerization process that allows precise control of molecular architecture. Unlike standard batch production, we can tailor the polymer chain to have specific branching and charge distribution, resulting in enhanced bridging capability and resistance to shear. This molecular design enables faster floc formation and denser sludge, improving downstream dewatering efficiency. As a forward-thinking PAM chemical manufacturer, we offer custom grades that reduce dosage by up to 30%, cutting operational costs while improving water quality. Our R&D team continuously explores one-pot synthesis and solvent-free methods, reducing environmental impact without compromising performance. We invite clients to scrutinize our technical specs—you will see the difference in molecular weight consistency and dissolution profile. These features are particularly valuable in high-throughput industrial plants where every percentage point matters.
AI-Integrated Quality Assurance

AI-Integrated Quality Assurance

We have embedded AI and machine learning algorithms into our manufacturing process, setting a new industry standard for a PAM chemical manufacturer. Real-time sensors monitor polymerization parameters such as temperature, viscosity, and molecular weight distribution, allowing predictive adjustments to maintain batch uniformity. This digitalization ensures that each batch meets the exact specifications, eliminating the typical variation from production runs. Consequently, our customers experience predictable performance, whether they use PAM for sludge dewatering or enhanced oil recovery. We also use AI to analyze user application data, providing recommendations to optimize flocculant usage and reduce waste. This smart manufacturing approach minimizes defects and raw material loss, contributing to sustainable production. By partnering with us, you gain access to our digital support platform, where you can track your orders and access quality analytics in real time.